 HAOCOOL
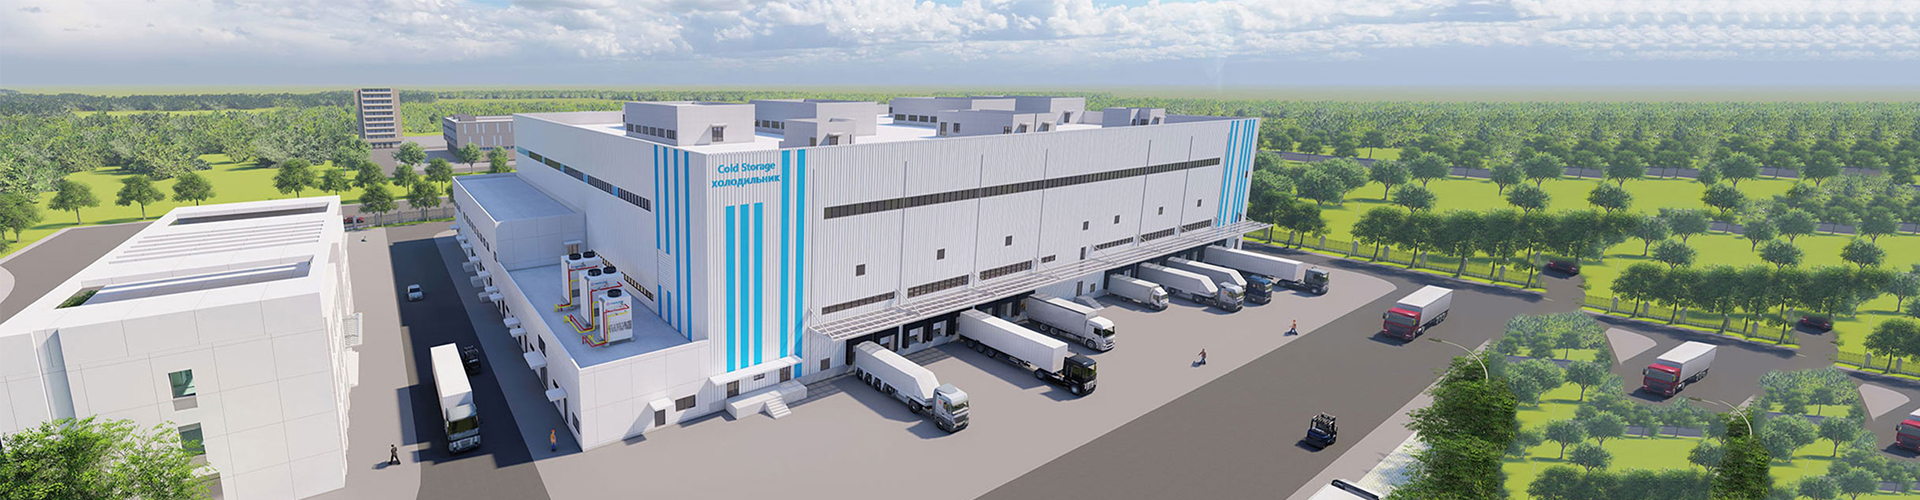
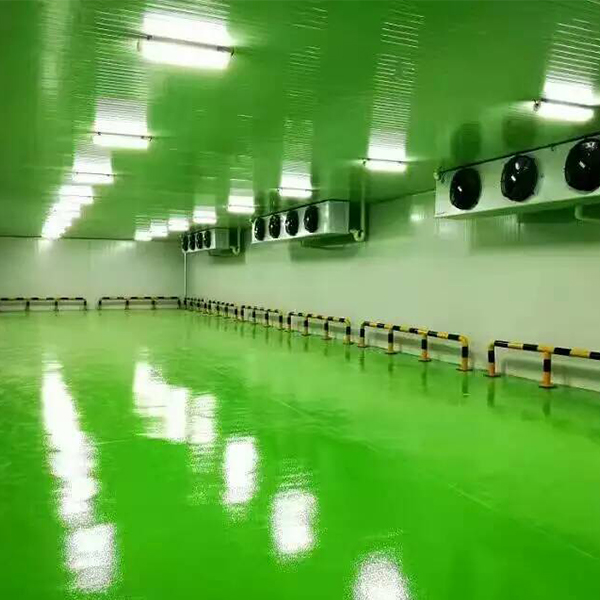
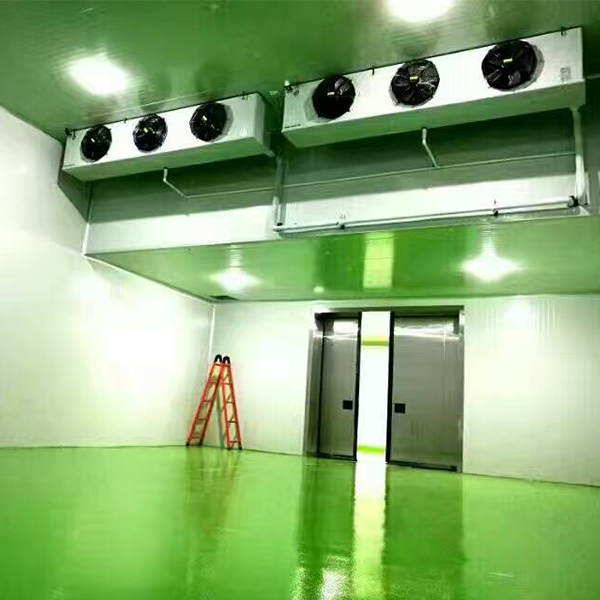
Beijing Coca-Cola Beverage Cold Storage Project
Case Details
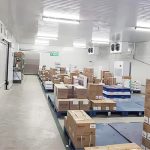
The Beijing Coca-Cola Beverage Cold Storage Project is a professional food and beverage refrigeration project constructed by HAOCOOL for the storage of finished Coca-Cola beverage products.
The project was completed in October 2016, with a construction period of approximately 30 days. The cold room was designed to provide stable temperature conditions, reliable refrigeration performance, and advanced automatic monitoring for finished beverage storage.
HAOCOOL had previously participated in several Coca-Cola refrigeration projects in Wuhan and Beijing, including cold rooms for syrup, raw materials, and other temperature-sensitive products. The Beijing finished beverage cold storage project successfully passed acceptance upon completion and demonstrated the company’s engineering capability in large-scale food and beverage refrigeration.
Project Information
| Parameter | Project Details |
|---|---|
| Project Name | Beijing Coca-Cola Beverage Cold Storage Project |
| Project Location | Beijing, China |
| Customer | Coca-Cola |
| Project Type | Food Cold Storage / Beverage Cold Room / Finished Product Cold Storage |
| Main Application | Storage of Finished Coca-Cola Beverages |
| Construction Period | Approx. 30 Days |
| Cooperation Year | 2016 |
| Completion Date | October 2016 |
| Refrigeration Method | Environmentally Responsible Fluorocarbon Refrigeration |
| Compressor System | Semi-Hermetic Reciprocating Air-Cooled Units |
| Compressor Brand | BITZER, Germany |
| Evaporator Brand | High-Quality German Refrigeration Equipment |
| Control System | Full PLC Automatic Control |
| Backup Design | Duty/Standby Automatic Switching |
| Monitoring | Temperature & Humidity Monitoring |
| Alarm System | High-Temperature SMS, Audible & Visual Alarm |
Beverage Cold Storage Solution
Finished beverage products require stable storage conditions to maintain product quality and support efficient warehouse distribution.
For the Beijing Coca-Cola project, HAOCOOL developed a complete beverage cold storage solution integrating refrigeration equipment, evaporators, PLC controls, temperature and humidity monitoring, alarm systems, and automatic backup operation.
The system was designed not only to maintain the required cold room environment but also to improve operational reliability and reduce the risk of refrigeration interruption.
This makes the project suitable as a reference for beverage factories, soft drink manufacturers, bottled drink warehouses, food distribution centers, and finished product cold storage facilities.
BITZER Semi-Hermetic Refrigeration System
The refrigeration system uses German BITZER semi-hermetic reciprocating air-cooled condensing units.
BITZER compressors are widely used in commercial and industrial refrigeration applications due to their stable performance, durability, and compatibility with professional cold storage systems.
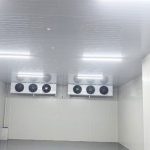
The evaporators were selected from high-quality German refrigeration equipment to provide efficient heat exchange and uniform air circulation inside the beverage storage area.
| Refrigeration Component | Configuration |
|---|---|
| Compressor | BITZER Semi-Hermetic Reciprocating Compressor |
| Condensing Method | Air-Cooled |
| Evaporator | German Refrigeration Air Cooler |
| System Configuration | Duty + Standby |
| Refrigeration Type | Fluorocarbon Refrigeration |
| Main Application | Finished Beverage Storage |
Duty and Standby Refrigeration Design
One of the key features of the project is the one-duty-one-standby refrigeration configuration.
Under normal operating conditions, one refrigeration unit performs the main cooling function while the second unit remains available as backup. The system can automatically rotate operating units and switch to the standby unit if a fault is detected.
This configuration provides several advantages:
- Higher refrigeration reliability
- Reduced risk of temperature interruption
- Automatic fault switching
- Balanced equipment operating hours
- Improved maintenance flexibility
- Better protection for stored products
For food and beverage manufacturers, system redundancy is particularly valuable because temperature control must remain stable even during equipment maintenance or unexpected faults.
Full PLC Automatic Control System
The complete refrigeration system uses a PLC-based automatic control platform.
The PLC system manages refrigeration equipment operation, temperature control, equipment rotation, fault detection, and alarm functions.
Temperature and humidity monitoring are integrated into the control system, allowing operators to continuously supervise storage conditions.
If the cold room temperature exceeds the preset limit, the system can activate:
- SMS alarm notifications
- Audible alarms
- Visual warning signals
- Equipment fault alerts
This intelligent monitoring system improves warehouse management efficiency and allows operators to respond quickly to abnormal operating conditions.
Environmentally Responsible Refrigeration Design
The Coca-Cola beverage cold storage project uses a fluorocarbon-based refrigeration system designed according to the environmental and technical requirements of the project.
The combination of reliable compressors, efficient evaporators, automatic control, and monitoring technology provides stable refrigeration performance while supporting efficient cold storage operation.
Project Results
The Beijing Coca-Cola Beverage Cold Storage Project was completed within approximately 30 days and successfully passed project acceptance.
Through the integration of BITZER semi-hermetic refrigeration units, German evaporators, duty/standby redundancy, PLC automatic control, temperature and humidity monitoring, and intelligent alarm systems, HAOCOOL delivered a reliable finished beverage storage solution for Coca-Cola.
The project provides a practical reference for beverage cold storage, finished product warehouses, soft drink factories, food cold rooms, beverage processing facilities, and industrial refrigerated distribution centers.
Product Recommendation
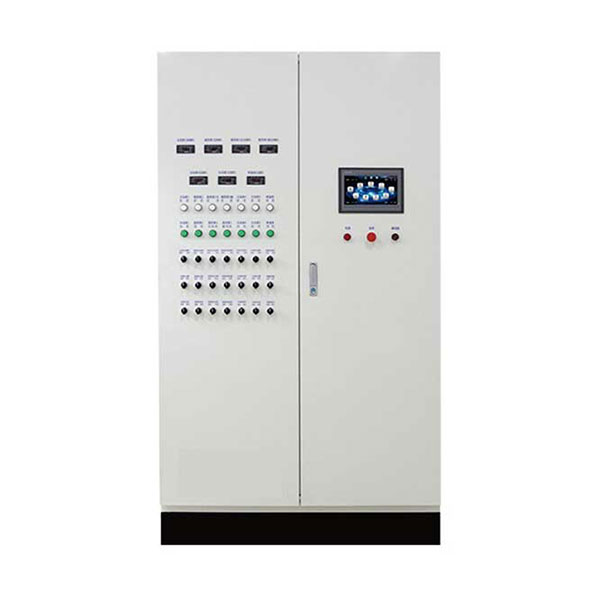
Cold Storage PLC Electrical Control Panel
Cold Storage PLC Electrical Control Panel A cold storage PLC electrical control panel is an intelligent control system designed to manage and monitor refrigeration equipment in cold rooms, freezer warehouses, food processing facilities, and industrial cold chain projects. By integrating PLC control technology with refrigeration componen...
View details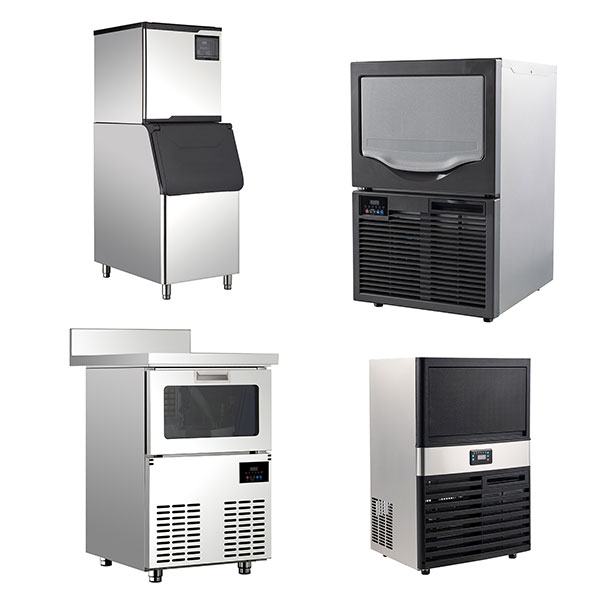
Ice Machine for Cold Storage and Cold Chain Facilities
Ice Machine for Cold Storage and Cold Chain Facilities An industrial ice machine is an important auxiliary equipment solution for seafood processing, fish markets, food distribution centers, agricultural logistics, and cold chain facilities. It produces a continuous supply of ice for rapid cooling, product preservation, transportation, ...
View details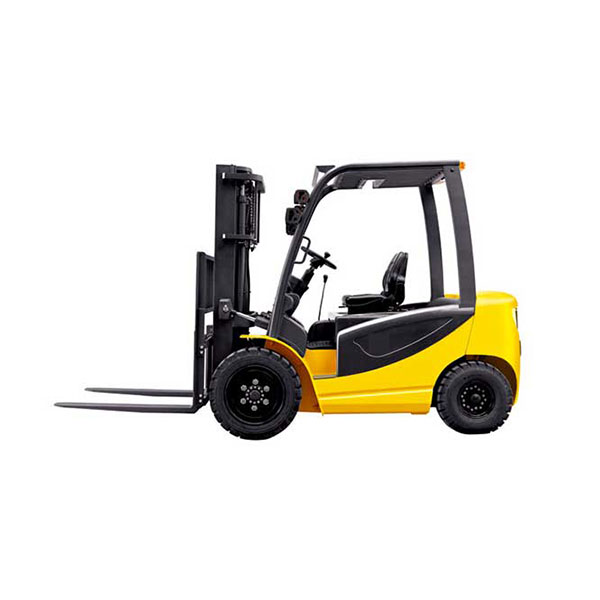
Cold Storage Forklift
Cold Storage Forklift A cold storage forklift is a specialized material handling solution designed for refrigerated warehouses, freezer rooms, food processing facilities, and cold chain logistics centers. Unlike standard warehouse forklifts, cold storage forklifts are designed to operate reliably in low-temperature and humid environment...
View details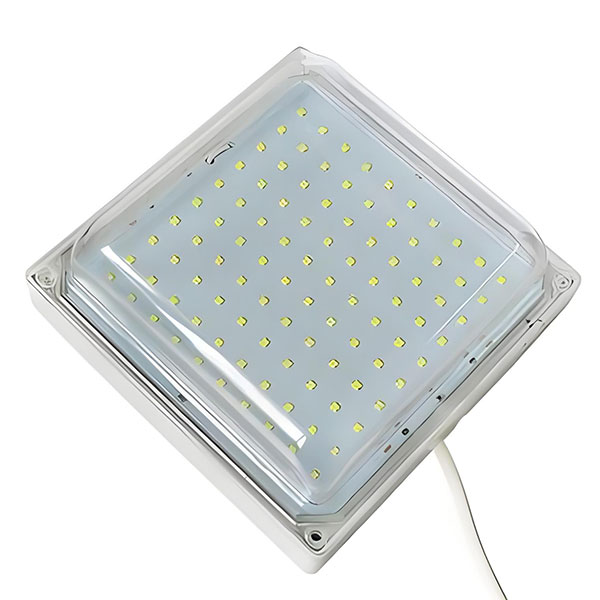
Cold Storage LED Light
Cold Storage LED Light Cold storage lighting is an essential part of modern refrigerated warehouses, freezer rooms, food processing facilities, and cold chain logistics centers. Unlike conventional indoor lighting, cold storage lights need to operate reliably in low-temperature, high-humidity, and potentially condensation-prone environm...
View detailsNEWS INFORMATION
 READ MORE
HAOCOOL Participates in AGRILINK 2026 in the Philippines, Showcasing Advanced Cold Storage and Cold Chain Solutions
0Building Connections in Southeast Asia and Supporting Modern Agricultural Cold Chain Development From October 8 to 10, 2026, HAOCOOL participated in AGRILINK – Agrilink Foodlink Aqualink, one of the leading agricultural, food, and aquacult...
-
READ MORE
How to Determine the Low-Temperature Storage Temperature for Hazardous Chemicals?
0The storage temperature of hazardous chemicals is not determined simply by choosing a lower temperature. It should be established according to the specific chemical properties, safety data, storage requirements, and applicable regulations. For...
-
READ MORE
What Is the Difference Between a Hazardous Goods Cold Storage Facility and a Standard Cold Storage Warehouse?
0Cold storage facilities are widely used for food, pharmaceuticals, chemicals, and other temperature-sensitive products. However, a hazardous goods cold storage facility has significantly different design and safety requirements from a standard...
-
READ MORE
Which costs more to build: a cold storage warehouse, a freezer warehouse, or a blast freezing warehouse?
0When planning a cold storage facility, users often compare the construction costs of cold storage warehouses, freezer warehouses, and blast freezing warehouses. Assuming similar storage capacity, building conditions, equipment brands, and cons...
-
READ MORE
Why Are the Requirements for Medical Cold Chain Warehousing Higher?
0The question of why medical cold chain warehousing demands higher standards frequently arises in the contexts of pharmaceutical distribution, vaccine storage, and the management of in vitro diagnostic reagents. Medical products are highly sens...
-
READ MORE
How to Achieve Energy Efficiency in Cold Storage? Practical Tips for Cold Chain Enterprises to Save Power and Reduce Consumption
0For cold chain enterprises, achieving energy efficiency in cold storage is a crucial factor in controlling operating costs. Since cold storage facilities operate continuously, electricity bills often account for a significant portion of daily ...
loading...
已经是到最后一篇内容了!